Industrial Rigging Hardware & Lifting Assemblies: Technical Specifications, Load Dynamics, and Assembly Standards

Industrial lifting and rigging assemblies serve as the primary structural link between overhead hoisting machinery and heavy payloads. Operating across mining shafts, offshore marine decks, structural steel erection, and heavy manufacturing plants requires matching specific hardware metallurgy, sling configurations, and termination styles to the precise mechanical stresses of each lift.
Selecting between alloy chain, steel wire rope, synthetic web slings, and forged connection hardware requires an evaluation of tensile capacity, bend radius efficiency, working temperature windows, and environmental resistance.
1. Alloy Steel Chain Systems & Components (Grade 80, 100 & 120)
Alloy steel chains are engineered for environments characterized by sharp edge profiles, severe abrasion, and high thermal exposure.
Metallurgy and Strength Characteristics
-
Grade 80 Alloy Chain (EN 818-2 / ASTM A391): Formulated from quenched and tempered nickel-chromium-molybdenum alloy steel. Nominal tensile stress at breaking force is $800\text{ N/mm}^2$ with an elongation threshold of at least 20% before failure, providing an engineered 4:1 safety factor.
-
Grade 100 Alloy Chain (EN 818-4 / ASTM A973): Utilizes specialized micro-alloy compositions delivering a tensile strength of $1000\text{ N/mm}^2$. Grade 100 provides roughly 25% higher Working Load Limit (WLL) over Grade 80 at identical nominal wire diameters.
-
Grade 120 Ultra-Alloy Chain: Features custom-profile cross-sections with flat contact surfaces that disperse unit bearing pressure, yielding up to 50% greater load capacity than Grade 80 while increasing structural stiffness against edge gouging.
Essential Chain Hardware Components
-
Master Links & Sub-Assemblies: Drop-forged alloy steel links designed to accommodate single, double, triple, or quad legs directly into crane hooks without binding or lateral pinching.
-
Mechanical Connecting Links (Hammerlocks): Two-piece clevis couplings joined via a hardened retaining pin and internal locking collar, certified to EN 1677-1 for modular assembly.
-
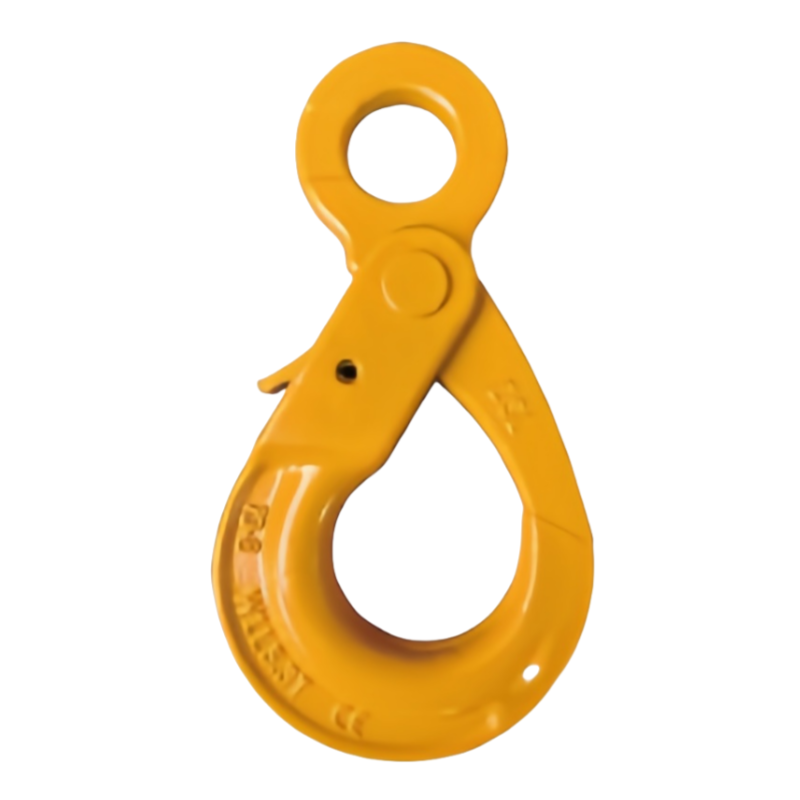
Self-Locking Clevis & Eye Hooks: Load-activated locking cams that automatically close under tension and cannot open while carrying payload weight.
-
Shortening Clutches & Clevis Grab Hooks: In-line chain shorten units that support 100% of the chain’s rated capacity without link deformation or point-loading.
2. Steel Wire Rope Slings & Swaged Terminations
Steel wire rope slings deliver high structural rigidity combined with predictable, multi-strand load sharing for structural civil engineering and heavy crane operations.
Stranding Classifications & Core Structures
-
6×19 Class (6×19S, 6×25Fi): Formed from 6 main strands containing 19 to 26 individual wires. Balances resistance to surface abrasion with bend endurance; standard for construction winch lines, general rigging chokers, and boom hoist lines.
-
6×36 Class (6×36WS, 6×41WS): Features 31 to 49 finer individual wires per strand. The higher wire density allows the rope to wrap tightly around sheaves, bollards, and sharp turns with reduced bending fatigue.
-
Core Types:
-
IWRC (Independent Wire Rope Core): A mini steel wire rope at the center that resists cross-sectional crushing under multi-layer spooling tension.
-
FC (Fiber Core): Sisal or synthetic core that absorbs and retains internal lubrication, improving flexibility for specific industrial hoist lines.
-
End Fitting Styles & Efficiency Ratings
The mechanical termination applied to wire rope dictates the assembly’s overall termination efficiency:
-
Flemish Eye with Swaged Steel Sleeve: The rope end is separated into two parts, woven back through itself to form an eye, and locked mechanically by pressing a carbon steel sleeve under thousands of tons of hydraulic pressure. Yields 100% termination efficiency.
-
Spelter Sockets (Poured Resin / Molten Zinc): Achieves 100% breaking efficiency; standard for long-term structural bridge stays, offshore mooring lines, and anchor pendants.
-
Wedge Sockets: Quick-disconnect mechanical fittings delivering 80% efficiency, used primarily on mobile crane hoist lines to allow rapid field shortening.
3. High-Strength Synthetic Slings: Flat Web & Round Slings
Synthetic slings are fabricated from continuous filament synthetic fibers engineered for scratch-sensitive, polished, painted, or non-conductive lifting applications.
Technical Comparison of Synthetic Profiles
| Property / Parameter | Flat Woven Webbing Sling | Endless Polyester Round Sling |
| Manufacturing Norm | EN 1492-1 / ASME B30.9 | EN 1492-2 / ASME B30.9 |
| Material Composition | 100% High-Tenacity Polyester (PES) | Parallel Strand Polyester Core in Woven Sleeve |
| Design Safety Factor | 7:1 (CE) or 5:1 (ASME) | 7:1 (CE) or 5:1 (ASME) |
| Capacity Identification | Universal color coding + woven stripes | Universal color coding + continuous stitch marks |
| Stretch / Elongation | Approx. 3% at Working Load Limit | Approx. 2% at Working Load Limit |
| Thermal Range | $-40^\circ\text{C}$ to $+100^\circ\text{C}$ | $-40^\circ\text{C}$ to $+100^\circ\text{C}$ |
| Surface Wear Mechanics | Outer web fibers bear direct tension | Outer jacket takes all abrasion; core remains isolated |
Edge Protection & Anti-Cut Accessories
Because synthetic fibers are vulnerable to shearing forces on unrounded metal corners, rigging operations integrate:
-
Polyurethane (PU) Protective Sleeves: Slide over the sling body to absorb sliding friction during choke hitches.
-
Kevlar & Dyneema Corner Protectors: Engineered pads placed between the load edge and sling body that withstand direct mechanical cuts under high corner loading.
4. Drop-Forged Rigging Hardware & Tensioning Systems
Forged hardware connections must withstand extreme cyclical stress, dynamic impact spikes, and harsh environmental exposure without undergoing brittle fracture.
Anchor & Chain Shackles (Crosby Type G-209, G-210, G-2130, G-2150)
-
Body & Pin Architecture: Quenched and tempered drop-forged carbon steel bows matched with heat-treated alloy steel load pins.
-
Screw Pin vs. Bolt-Type Safety Shackles:
-
Screw Pin Shackles: Quick assembly for non-permanent rigging; susceptible to backing out under rotational line movement.
-
Bolt-Type Safety Shackles (Hex Bolt, Nut & Cotter Pin): The required hardware standard for long-term installations, underwater rigging, and lifts that rotate or cycle continuously.
-
-
Corrosion Protection: Hot-Dip Galvanizing (HDG) per ASTM A153 delivers a 60–85 micron zinc layer for marine and offshore installations.
Heavy-Duty Industrial Turnbuckles (US Fed Spec FF-T-791b)
Turnbuckles provide precision tensioning and line length adjustment for architectural bracing, structural towers, and cargo tie-downs:
-
End Fittings: Jaw & Jaw, Eye & Eye, Hook & Hook, or mixed combinations. Jaw terminations provide zero-slip pinned retention on pad eyes, while eye ends accept standard shackle bows.
-
Material Ratings: Quenched and tempered drop-forged steel bodies with UNC-rolled threads for gall-free operation under heavy tension loads.
Drop-Forged Wire Rope Clips (G-450 Style)
-
Construction: Heavy drop-forged steel saddles conforming to US Federal Specification FF-C-450 Type 1 Class 1, paired with U-bolts and hex nuts.
-
Installation Standard: Must be installed with the saddle resting directly on the live (load-bearing) side of the rope—“never saddle a dead horse”—to prevent crimping the primary tension line.
5. Engineering Dynamics: Tension Calculations & Angle Reductions
Calculating sling capacity requires determining the horizontal sling angle formed between the sling leg and the payload surface.
Load Angle Multipliers
When two or more sling legs share a load ($W$), the actual tension ($T$) induced along each leg increases sharply as the horizontal angle ($\theta$) decreases:
At a 30° horizontal angle, the tension experienced by each individual sling leg equals 100% of the entire payload’s weight.
Request Technical Data Sheets & Sourcing Specifications
Have specific project parameters, CAD drawing requirements, or bulk hardware bills of materials to review?
-
Specify Load Parameters: Working load limit (WLL), required design factor (4:1, 5:1, or 7:1), nominal diameter, and reach length.
-
Define Environmental Constraints: Ambient operating temperatures, chemical exposure profiles, and required surface coatings (HDG, zinc plating, thermal diffusion, or stainless steel).
-
Access Full Test Data: Receive certified proof-load charts, dimensional diagrams, and material test certificates for all standard and custom rigging configurations.